 English
 العربية
 Bosanski jezik
 Čeština
 Dansk
 Nederlands
 Wikang Filipino
 Suomi
 Français
 Deutsch
 Magyar
 Íslenska
 Bahasa Indonesia
 Italiano
 日本語
 한국어
 Bahasa Melayu
 Polski
 Português
 Русский
 Cрпски језик
 Español
 ภาษาไทย
 Türkçe
 Tiếng Việt

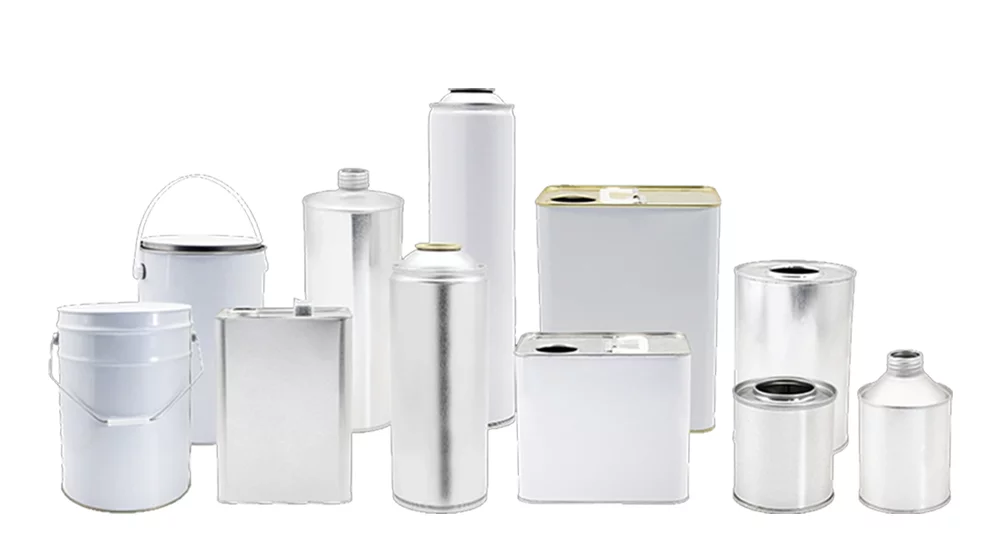
Aluminum Cans might look like the same shiny shell to most folks, but for OEM buyers dealing in chemicals, aerosols, or industrial-grade food packaging—it’s a whole different ballgame. From alloy mixes that don’t play nice with recycling systems to sneaky internal coatings that muck up the process, not all cans pull their weight when it comes time to toss ‘em in the blue bin. And if you’re wrangling ESG goals or facing down compliance audits? You’d better know what’s inside your can—literally.
“It’s not just about recyclability,” says Chen Wei, senior materials engineer at FANXUN (2024 Q1 Materials Integrity Report). “It’s about performance under pressure—burst tests don’t lie.”
Reading Notes on the Real Deal Behind Aluminum Cans
➔ Internal Coatings & Recycling: Epoxy phenolic lacquer protects contents but complicates recycling due to difficult separation from base metal.
➔ Recycled Content Value: Higher recycled aluminum percentages reduce energy demand by up to 95%, offering both environmental and cost benefits.
➔ Dimensional Influence: Wall thickness, dome depth, and neck diameter all affect recyclability efficiency in processing plants.
➔ Chemical Resistance Testing: Essential for ensuring cans won’t contaminate recycling streams or fail under pressure post-reuse.
➔ Regulatory Compliance: Standards like REACH and RoHS are crucial for legal operations and market access with recycled materials.
Aluminum Cans: Understanding The Recycling Process
Let’s break down how aluminum cans go from your hand to a new product—clean, tested, and ready to roll again.

How Internal Coatings Affect Recyclability of Aluminum Cans
- Internal coatings like epoxy phenolic lacquer are used to protect the can’s contents from reacting with the metal.
- These internal coatings often contain polymers such as BPA, which don’t melt with aluminum and must be separated before recycling.
- If not removed properly, these coatings become a contaminant that reduces the overall recyclability of aluminum cans.
- Some facilities use pyrolysis or chemical stripping methods to deal with this challenge, but not all plants are equipped for it.
- The presence of coating materials can lower the value of scrap aluminum or lead to its rejection by buyers.
The Role of Recycld Aluminum Content Percentage in Sustainability
| Material Type | Energy Used (kWh/kg) | CO₂ Emissions (kg CO₂/kg) | Recycling Rate (%) |
|---|---|---|---|
| Primary Aluminum | 14.5 | 11.5 | — |
| Recycled Aluminum | 0.7 | 0.5 | 73% |
| Mixed Scrap Sources | 3.2 | 2.8 | Varies |
Using more recycled aluminum slashes energy consumption and lowers your carbon footprint big time. A higher content percentage means less mining and refining of raw primary aluminum, which is energy-hungry and dirty work. It’s not just about saving power—it’s about cutting emissions too. Life cycle assessments show that upping recycled content makes a serious dent in environmental impact.
Dimensions That Impact the Aluminum Can Recycling Process
• Wall thickness matters—a thinner wall melts faster but might tangle during processing
• Dome depth affects how well cans compact during transport, influencing fuel costs
• Odd shapes or sizes? They mess with sorting tech like eddy current separators
• Uniformity across batches ensures smoother rides through automated sorting lines
Those tiny details in design? They’re huge when it comes to speeding up or slowing down the entire recycling process for aluminum cans. Even consumer behavior plays a part—crushed vs uncrushed cans change how they’re picked up by machines.
Testing Standards for Recycled Aluminum Quality Assurance
Recyclers don’t just melt and hope for the best—they test every batch:
- Burst pressure tests check if recycled material holds up under stress
- Chemical resistance testing ensures no weird reactions when reused in food-grade packaging
- Spectrometry confirms correct alloy composition, avoiding unwanted mixes that weaken strength
- Mechanical testing measures tensile strength and ductility
These tests follow strict protocols like those outlined in various ASTM standards, making sure that even after multiple recycling loops, your soda can stays safe, strong, and shelf-ready.
5 Ways Aluminum Cans Benefit The Environment

Cracking open a cold drink might feel small, but those little aluminum cans pack a serious punch for the planet.
Energy Savings: The Impact of Recycled Aluminum on Production
Recycling just one aluminum can saves enough energy to run a TV for three hours. Now imagine that multiplied by billions—yeah, it adds up fast.
✔️ Energy efficiency is where recycled aluminum shines. It slashes energy use by up to 95% compared to creating new metal from raw bauxite. That’s not just impressive—it’s game-changing.
✔️ Lowering production costs is another big win. Less energy means cheaper manufacturing and fewer emissions belching into the air from factories.
✔️ Oh, and let’s not forget the massive drop in carbon emissions, which helps curb climate change while keeping your soda fizzy and guilt-free.
Here’s how energy stacks up when using recycled vs. virgin aluminum:
| Process Type | Energy Used per Ton | CO₂ Emissions per Ton | Cost Reduction (%) |
|---|---|---|---|
| Virgin Aluminum | 14,000 kWh | 12 tons | 0% |
| Recycled Aluminum | ~700 kWh | <0.5 tons | Up to 95% |
So yeah—next time you toss that can into the blue bin? You’re basically fighting climate change with style.
Reduced Waste: Why Material Type Matters in Recycling
Some stuff breaks down, some stuff doesn’t—and some things like aluminum cans keep coming back stronger every time.
• Unlike plastic, aluminum doesn’t lose quality after recycling. Its solid material properties mean it can be reused indefinitely without degrading—a rare trait that makes it a recycling superstar.
• High recycling rates for aluminum—often over 60% globally—mean fewer cans clogging landfills or floating around oceans pretending they’re fish food.
• With landfill space shrinking fast, using materials like aluminum that avoid long-term waste buildup is a no-brainer for smart packaging choices.
Each year, choosing better materials could mean millions fewer tons of garbage piled sky-high behind cities or dumped into rivers—and that’s something we can all get behind without hugging trees awkwardly at parties.
The Ecological Footprint of Aluminum Cans: A Closer Look
Let’s break this down quick so you see why those shiny silver cylinders are secretly eco-warriors:
🔹 They reduce overall resource depletion, since recycling uses way less water and raw material than mining new ore.
🔹 Their lower total ecological footprint means fewer emissions across their entire life cycle—from production to disposal.
🔹 Thanks to their small size and high recyclability, they support urban sustainability goals without needing fancy tech or major infrastructure changes.
🔹 Life cycle assessments show they outperform many alternatives when factoring in transport weight, reusability, and end-of-life processing.
🔹 Their minimal contribution to long-term waste helps cut back on environmental degradation caused by non-recyclable packaging options.
🔹 And let’s not forget—they’re lightweight as heck! Less fuel burned during shipping = lower overall carbon footprint, which is always welcome news for our overheating planet.
So yeah—whether it’s about saving resources or shrinking your impact silently while sipping soda at the beach—those humble cans are doing way more than holding your drink together.
Are All Aluminum Cans Recyclable? Discover The Truth

Ever wondered if all those shiny aluminum cans in your bin are equally recyclable? Let’s break it down and see what really makes the difference.
Comparing Different Alloy Grades: Are They All Recyclable?
Not all aluminum alloys are created equal—some go through the recycling process like butter, others cause real headaches. Here’s how different alloy grades stack up:
- 1000 Series: Nearly pure aluminum, super easy to recycle thanks to its simple metal composition.
- 3000 Series: Common in beverage cans; contains manganese, which doesn’t interfere with recyclability.
- 5000 Series: Magnesium-based alloys, often used in industrial applications—not ideal for can recycling due to contamination risk.
- 6000 Series: Includes silicon and magnesium; good strength but can complicate melting processes during recycling.
- Cast aluminum alloys (like 7000 series) are a no-go—they contain zinc and other elements that degrade quality when mixed with can-grade material.
It all boils down to how each alloy reacts under heat and separation. The more uniform the alloy family, the smoother the ride through the recycling process. So while most consumer-facing cans fall within recyclable ranges, mixing them with incompatible types messes with the entire system.
Why Chemical Resistance Testing is Crucial for Recyclability
When it comes to recycling aluminum cans, it’s not just about tossing them into a blue bin. There’s a chemical side to this story that most folks miss.
• Coatings used on cans need to withstand acidic drinks—but those same coatings might resist breakdown during reprocessing.
• If a coating clings too tightly or releases toxic compounds when heated, it ruins batches of recycled metal.
• That’s why rigorous testing for things like corrosion resistance and polymer stability is key before approving any new can design.
A 2024 report from the International Aluminum Institute noted that “up to 12% of rejected batches stemmed from coating-related contamination.” That’s huge—and totally avoidable if proper tests are done upfront.
So while you might think of your soda can as just metal, there’s a lot more going on beneath that glossy finish. Proper testing ensures we don’t end up recycling trash into more trash—because nobody wants junk metal coming back as your next drink container.
The Economic Impact Of Aluminum Can Recycling

Recycling aluminum cans doesn’t just help the planet—it makes serious business sense. Let’s break down how.
Cost Implications of Recycled Aluminum Content in Manufacturing
Mixing recycled metal into production lines isn’t just eco-friendly—it’s wallet-friendly too.
- Using recycled aluminum cuts overall manufacturing costs, especially when energy prices spike.
- Sourcing scrap locally avoids global fluctuations in raw material prices, giving factories more price control.
- Less energy is needed to process recycled metal—up to 95% less—so energy consumption drops significantly.
Now, pair that with better production efficiency, and you’ve got a cost-saving engine humming along. Brands that embrace this shift often see a measurable return within months. That’s why companies like FANXUN are leaning into recycling, blending savings with sustainability without skipping a beat.
The Value of Compliance: Regulatory Standards in Aluminum Recycling
Meeting rules isn’t just red tape—it unlocks doors and protects your bottom line.
• Following major frameworks like REACH or RoHS means smooth entry into global markets.
• Staying compliant reduces risk exposure from fines or trade restrictions tied to non-compliance.
• Aligning with environmental norms strengthens brand trust and reputation.
Grouped benefits:
– Legal Access: Compliance ensures uninterrupted participation across regulated markets like the EU and Japan.
– Financial Efficiency: Avoids costly penalties while streamlining internal processes around waste handling.
– Strategic Advantage: Demonstrates leadership in sustainable practices, attracting eco-conscious partners and investors.
All told, the real win here is long-term resilience for any player in the recycling industry, especially those navigating complex international supply chains involving millions of tons of used aluminum cans annually.
Pallet Configuration and its Effect on Shipping Costs
How you stack it? Yeah, it matters—a lot more than most think.
Smart pallet layout boosts both warehouse space use and truckload density. When optimized, fewer shipments are needed—cutting down on fuel bills fast. That’s where solid thinking around pallet configuration comes into play.
Efficient stacking shrinks your carbon footprint while improving your entire logistics game—from packaging design to delivery routes. Even minor tweaks can reduce total shipping costs, making a big dent over time.
In today’s tight-margin world, every inch counts—and every dollar saved adds up when moving thousands of bulk-packed beverage-grade recyclable containers made from lightweight yet durable aluminum materials.
Steps To Properly Recycle Aluminum Cans
Recycling aluminum cans right isn’t rocket science, but it sure helps to follow the correct order. Here’s how to do it without missing a beat.

Sorting Aluminum Cans: Dimensions and Quality Standards
Start with the basics—get your aluminum cans sorted by size and cleanliness.
• Crushed or dented? Toss ’em into the damaged pile.
• Uniform sizes make processing faster and smoother.
• Remove anything with mixed materials like plastic labels or foil seals.
- Check for visible contamination—sticky residues or food leftovers are a no-go.
- Use a simple gauge tool to measure can height and diameter for batch sorting.
- Separate beverage-grade cans from industrial-use ones to maintain material consistency.
→ Don’t mix in steel or tin containers—that throws off the whole recycling game.
According to a 2024 report by the Global Recycling Insights Institute, “Contamination during initial sorting reduces material recovery efficiency by up to 17%, especially in urban collection centers.” That’s real money being lost—and unnecessary waste.
Preparing Cans for Recycling: Importance of Surface Finish
Clean cans aren’t just nice—they’re essential for recycling quality.
- Soap and water go a long way in removing sugars, oils, or other gunk.
- Avoid abrasive scrubbing; you want that surface finish intact.
- A clean surface means fewer impurities when melting down, which equals better alloy quality later on.
Multiple short steps help here:
- Rinse each can thoroughly inside out.
- Let them air dry completely—moisture leads to corrosion.
- If you see paint residue or sticky glue, scrape gently without damaging the aluminum layer underneath.
A smooth surface finish ensures lower melting point fluctuations during reprocessing, which is key when scaling operations like those at FANXUN’s regional facilities across North America.
Proper Storage Conditions: Temperature and Humidity Factors
You’ve sorted and cleaned your aluminum cans, now don’t mess it up in storage.
- Keep them cool—ideally under 25°C.
- Humidity? Below 60% is your friend.
- Store indoors if possible; rain + metal = corrosion city.
Grouped tips:
🗸 Dry environment = longer shelf life before remelting
🗸 Avoid stacking wet cans—they’ll oxidize fast
🗸 Use breathable bins instead of sealed plastic bags
Excess heat speeds up oxidation, while high humidity invites mold growth around any leftover sugars inside unwashed cans—which makes them harder to recycle cleanly later on. Better safe than sorry!
Final Inspection: Burst Pressure Testing for Recycled Cans
Once your recycled batch is ready, time for one last check—the burst test.
• This test checks if your recycled aluminum cans can handle internal pressure without failing catastrophically (think soda explosion).
• It’s critical for safety compliance—especially if you’re planning reuse in carbonated beverages or pressurized contents.
Steps involved:
- Fill sample cans with water or inert gas under controlled conditions.
- Slowly increase internal pressure until failure occurs—or doesn’t!
- Record data points like maximum PSI tolerated before rupture.
This final inspection ensures structural integrity meets modern safety standards—a must-have step before sending those shiny new containers back into circulation as part of a closed-loop recycling system that actually works.
FAQs about Aluminum Cans
What internal coatings are used in aluminum cans, and how do they affect recyclability?
Inside most aluminum cans lies a thin protective layer—often an epoxy-based coating—that keeps beverages from reacting with the metal. It’s invisible but essential. The challenge? These coatings don’t just vanish during recycling. They burn off at high temperatures, releasing gases that must be carefully managed to avoid contaminating the recycled metal. While not impossible to handle, this extra step adds complexity and cost.
How does recycled aluminum content percentage impact sustainability efforts?
- Using recycled aluminum slashes energy use by up to 95% compared to producing new material from ore
- Less mining means fewer scars on landscapes and reduced water pollution
- Helps companies meet strict environmental rules like REACH or RoHS without major overhauls
The higher the recycled content, the more sustainable—and often more affordable—the production process becomes.
Why is burst pressure testing critical before shipping recycled metal containers?
Burst pressure testing isn’t just a box-ticking exercise—it’s what stands between safe delivery and disaster. Picture thousands of aerosol cans under stress in a hot truck bed; one weak seal could rupture under heat or altitude changes. Testing ensures each container can withstand real-world conditions: compression during transport, sudden jolts on conveyor belts, even temperature swings in warehouses.
It’s peace of mind for manufacturers—and safety insurance for everyone else down the line.
Do temperature and humidity matter when storing empty aluminum containers pre-filling or pre-shipment?
Absolutely—they matter more than most realize. Humidity invites corrosion if moisture sneaks past packaging layers; extreme cold can make certain alloys brittle over time; too much heat may warp surface coatings meant for later printing or labeling.
Keeping storage areas dry and climate-controlled preserves both appearance and performance—because no one wants their product compromised before it even gets filled.
References
- Aluminum Cans – FANXUN
- Burst Testing for Packages (ASTM F2054) – Industrial Physics
- BPA In Cans – Do All Tins Contain Bisphenol A? – uCan-Packaging
- Advanced Aluminum Recycling Cuts Production Energy Use Ninety-Five Percent – Sustainability Directory
- Eddy Current Aluminum Can Separator – Made-In-China Insights
- Burst Testing Standards – Westpak
- Production Manufacturing – FANXUN
- Various Aluminum Alloy for Manufacturing – 3ERP
- Aluminum: Material-Specific Data – US EPA
- Global Aluminium Scrap Export Restrictions (Carbon Footprint) – Discovery Alert
- Aluminum Alloy Overview – Alumeco
- REACH Compliance in Metal Recycling – Okon Recycling
- RoHS Directive – Alumeco