 日本語
 English
 العربية
 Bosanski jezik
 Čeština
 Dansk
 Nederlands
 Wikang Filipino
 Suomi
 Français
 Deutsch
 Magyar
 Íslenska
 Bahasa Indonesia
 Italiano
 한국어
 Bahasa Melayu
 Polski
 Português
 Русский
 Cрпски језик
 Español
 ภาษาไทย
 Türkçe
 Tiếng Việt

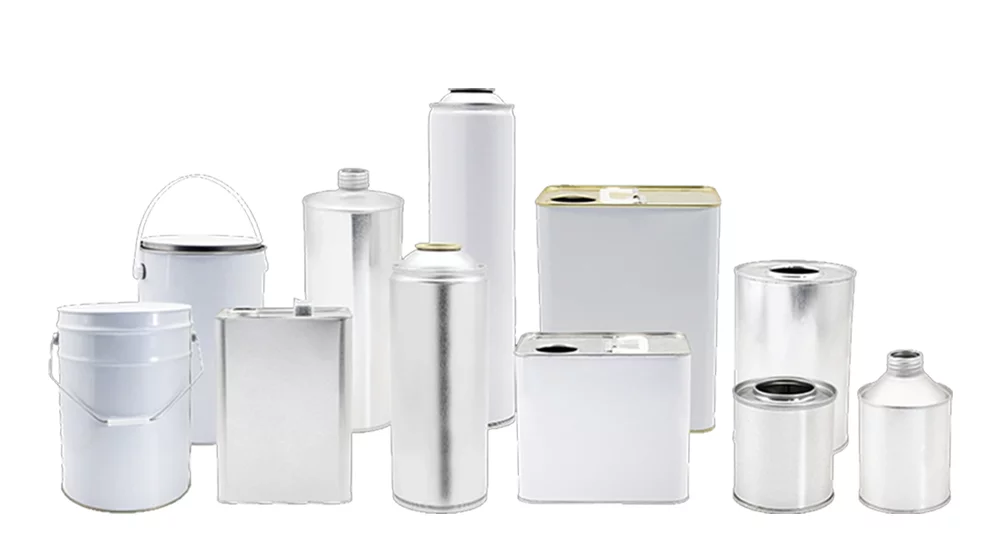
Tinplate cans may look simple, but a single seam defect or lacquer mismatch quickly turns a smooth production run into palletized waste. At industrial scale, microscopic flaws compound rapidly.
This guide outlines core manufacturing specs—chemistry, 推進剤の適合性, gauge tolerances, seam overlap, and crimp depth—while establishing testing and logistics protocols to ensure product integrity.
Key Points for Tinplate Cans Reliability
➔ Material Specs: Electrolytic tin coating (1.1–8.4 g/m²), precise steel gauge, and compatible internal lacquer ensure optimum corrosion resistance and pressure tolerance.
➔ Seam Precision: High-frequency side seam welding and double‐seam crimping integrity prevent micro-leaks and withstand aggressive internal propellant pressures.
➔ テストプロトコル: UN/DOT compliant 50°C water bath leak tests and burst pressure validation confirm seam integrity and valve reliability.
➔ Logistics Best Practices: Engineered palletization, コンテナ化, and strict dimensional checks safeguard the supply chain from factory to shelf.
Guided Introduction
Tinplate cans are ubiquitous, yet their engineering fundamentals require strict tolerances. This overview defines ブリキ, highlights critical physical properties, and identifies the structural components that endure the most stress.

Understanding Tinplate: Steel Substrate and Tin Coating Basics
産業 ブリキ comprises a cold-rolled スチール基板 electroplated with a thin, ユニフォーム 錫コーティング—a superior 材料構成 engineered for strict food-contact and pressure-handling environments.
- 電気めっき bonds 錫 onto the 鋼鉄 表面, achieving exact coating weights (typically E2.8/2.8 g/m²) for predictable performance.
- Specialized curing and passivation adjust コーティング porosity, dictating how tinplate cans resist aggressive brines, 酸, or sulfur compounds.
- Cut edges and micro-abrasions risk exposing bare 鋼鉄; 高度な 製造工程 actively account for this to neutralize rust risks.
While colloquially called “ブリキ缶,” コマーシャル ブリキ缶 rely on highly controlled layers and surface chemistry to function safely.
Key Material Traits: 耐食性, 成形性, and Gauge
The performance of tinplate cans depends on balancing three critical, competing プロパティ.
- 耐食性
- Drivers
- 錫コーティング density on the ブリキ
- BPA-IN or epoxy-phenolic internal lacquers matched to fill chemistry
- Watch-outs
- High porosity or pinholes causing rapid underfilm corrosive attack
- Drivers
- 成形性
- What it needs
- Specific temper grades (例えば。, T-3) 確保する 延性 for necking, ビーズ, そしてフランジ加工
- What it fights
- Excessive steel 強さ that induces micro-cracking during deep drawing
- What it needs
- ゲージ
- なぜそれが重要なのか
- Thicker gauge (0.20mm+) exponentially increases 耐久性 and burst pressure tolerance
- キャッチ
- Downgauging (例えば。, to 0.18mm) saves cost but requires bottom profiling to prevent transit denting
- なぜそれが重要なのか
コアコンポーネント: 缶本体, ドーム, Bottom End, and Side Seam
Each structural element carries specific mechanical loads. Weaknesses emerge when these components are misaligned.
- 缶本体
- Dictates wall ゲージ and total volumetric capacity.
- Absorbs tooling stress; demands high 成形性 and coating scuff resistance.
- ドーム そして bottom end
- Resist internal propellant pressure and prevent outward doming/paneling.
- Require rigid 構造 to prevent “oil-canning” deflection under load.
- Side seam
- In welded designs, high-frequency (500–600 Hz) side seams minimize heat-affected zones and coating burn-off.
- Micro-leak prevention is paramount; a singular defect compromises an entire batch of tinplate cans.
Optimal tinplate can design relies on precise tension: reinforced at pressure points, ductile during forming, and hermetically sealed.
💡 Ready to optimize your tinplate specifications? 以上で 30 years of canister manufacturing expertise, FANXUN が提供するのは、 1-当日の解決策提案 (デザインも含めて, 材料, そして引用符). カスタマイズサービスを詳しく見る or browse our ティンエアロゾル缶.
おお! Tinplate Cans Boost Your Packaging ROI
頭いい ブリキ specification—integrating advanced coatings, micrometer-accurate seams, and 175-LPI print resolution—transforms standard containers into high-performance assets. FANXUN leverages these metrics to systematically reduce scrap and drive reliable packaging ROI.

How Internal Lacquer Enhances Shelf Life and Brand Appeal
- ブリキ缶 require internal treatments strictly managed as high-grade food-contact surfaces.
- ラッカー そして 内部コーティング selection dictates performance:
- 耐食性
- Blocks metal-ion migration to preserve taste/color profiles, maintaining 製品の完全性.
- Serves as active 食品の保存 by halting oxidative reactions that degrade 貯蔵寿命.
- Consumer safety
- 完全に硬化, migration-compliant films guarantee Consumer safety during stringent regulatory audits.
- Appearance and trust
- High-density films prevent internal staining and haze, silently elevating Brand perception.
- クリーン, bright interiors telegraph freshness instantly to consumers.
- Technical targets for tin plate can specs:
| メトリック | 代表的なターゲット | なぜそれが重要なのか |
|---|---|---|
| 乾燥膜厚 (μm) | 6–12 | Reduces pinholes, ブースト 耐食性 |
| Cure peak metal temp (℃) | 190–210 | Improves cross-linking, lowers taint risk |
| Porosity (defects/100 cm²) | ≤2 | 守る 貯蔵寿命 そして 製品の完全性 |
FANXUN aligns specific lacquer chemistries to your payload—acidic food or aggressive aerosols—ensuring ブリキ缶 remain uncompromised.
Double Seam Integrity for Reduced Returns and Waste
Superior lithography cannot save a leaking container. 厳格な ダブルシーム execution is the foundation of Sealing integrity.
- 漏れ防止 basics
- Verify flange dimensions and seaming chuck profiles pre-run to eliminate silent Packaging defects.
- Treat internal pressure drops as seam geometry failures; utilize 品質管理 teardown metrics for root-cause analysis.
- Dial in process discipline
- Calibrate seamer lifter pressure to exact mechanical specifications.
- Execute teardowns continuously (start/middle/end) targeting >45% actual overlap.
- Document tightness ratings and wrinkle limits so Returns management has actionable QA data.
★ Maintaining micrometer-level seam consistency slashes Product spoilage, virtually eliminates scrap, and turns 廃棄物の削減 into a measurable financial asset. FANXUN engineers manufacturing around hermetic repeatability to permanently solve return issues.
Leveraging Lithography and Coating Application to Stand Out
Shelf impact requires maximum optical fidelity. リソグラフィー combined with specialized topcoats maximizes visibility for ブリキ缶.
Print that sells
- 150–175 LPI Printing technology と組み合わせた CTP (Computer-to-Plate) controls ensures sharp typography and vivid gradients, optimizing グラフィックデザイン.
- Strict densitometry limits color drift, 保護 パッケージングの美学 そして Market visibility across varying production lots.
- Protection that keeps the look intact
- コーティング塗布 and thermal cure
- High-slip over-varnishes increase scuff resistance, 確保する 視覚的な魅力 survives automated filling and transit.
- Superior rub-resistance mitigates retail damage and write-downs.
- ブランドの差別化
- Tactile varnishes, spot gloss, and matte contrasts signal premium positioning without structural retooling.
- Easy way to plan your pack look
- Define the visual architecture (マット, メタリックな, 高光沢).
- Align finishes with strategic ブランドの差別化.
- Standardize ink density and varnish coat weights for batch-to-batch uniformity.
FANXUN synchronizes premium lithography and protective varnishes, transforming ブリキ缶 into durable, high-impact brand assets.
🎨 Bring your brand to life with high-fidelity lithography. FANXUNさん 3 advanced Fuji printing lines and flexible minimum order quantities (starting from just 3,000 個) make premium packaging accessible. Contact us for free samples with a prototyping turnaround time of just ~10 days.
5 Steps To Safe Can Handling

Handling errors generate microscopic dents and internal micro-cracks that inevitably lead to failures. Implementing these five protocols protects your metal can line from unloading to storage. FANXUN integrates these standards to guarantee ブリキ缶 maintain absolute structural integrity.
ステップ 1: Inspect Seam Integrity and Valve Crimping
- Inspection process
- Initiate automated and manual 目視検査 to intercept obvious Can defects.
- Flag litho scratches, flange ripples, or lacquer fractures on ブリキ 体.
- Initiate automated and manual 目視検査 to intercept obvious Can defects.
- 縫い目の完全性
- Verify double seam parameters via micrometer and optical profiling.
- Treat sub-standard countersink depths as critical Seal quality 危険.
- Enforce strict adherence to 製造基準—rejecting marginal deviations.
- Verify double seam parameters via micrometer and optical profiling.
- バルブかしめ
- Measure crimp diameter and depth (typically 4.75mm – 5.00mm) circumferentially.
- Asymmetrical バルブかしめ causes slow-release propellant leaks that manifest weeks after filling.
- Measure crimp diameter and depth (typically 4.75mm – 5.00mm) circumferentially.
ステップ 2: Conduct Leak Testing and Pressure Testing
FANXUN applies destructive and non-destructive protocols to guarantee エアゾール缶 安全性.
- リークテスト
- Submerge units in 50°C–55°C UN-compliant water baths; これら Test methods maximize 漏れ検出.
- Micro-bubbles indicate immediate コンテナの完全性 failures requiring batch quarantine.
- 圧力試験
- Subject samples to burst testing (often requiring >15 bar tolerance).
- Strict pass/fail criteria rule: structural failure means shipment denial. 厳格な 品質保証 prevents liability.
ステップ 3: Manage Internal Pressure with Proper Propellant Compatibility
- 内圧
- Calculate phase-change pressure spikes at elevated warehouse temperatures (例えば。, 55°C/130°F).
- Thermal expansion rapidly turns safe volumes into burst hazards.
- Calculate phase-change pressure spikes at elevated warehouse temperatures (例えば。, 55°C/130°F).
- 推進剤の適合性
- Map hydrocarbon or compressed gas behavior against the lacquer to prevent chemical degradation and 化学相互作用.
- Continuously monitor Gas properties for vapor pressure stability.
- Map hydrocarbon or compressed gas behavior against the lacquer to prevent chemical degradation and 化学相互作用.
- Aerosol formulation
- 確認する Can contents are non-corrosive to the selected polymer lining.
- Anchor Pressure management strictly to UN/DOT 安全規格.
- Minute formulation shifts inside ブリキ缶 drastically alter pressure dynamics.
ステップ 4: Ensure Dimensional Accuracy Before Filling
Precision geometry is the baseline for automated 品質管理.
- Map exact 缶の寸法 using optical/laser Measurement tools, validating against CAD 仕様.
- Enforce strict Tolerances (例えば。, ±0.1mm) targeting:
- Overall body diameter and height,
- Neck-in reduction angles (例えば。, 211 に 209),
- 1-インチ バルブ aperture curl profiles.
- Deviating Container geometry crashes the 充填工程, destroying seaming chucks and causing jam-ups. FANXUN eliminates this via pre-shipment dimensional profiling of all ブリキ缶.
ステップ 5: Store with Correct Palletization and Bulk Delivery Practices
- パレット化
- Deploy interlocking stack patterns maximizing carton Edge Crush Test (ECT) limits to prevent side-wall deflection.
- Utilize heavy-duty corner boards to distribute forklift clamping forces.
- Deploy interlocking stack patterns maximizing carton Edge Crush Test (ECT) limits to prevent side-wall deflection.
- Storage practices
- Maintain climate-controlled environments preventing flash rust on exposed steel edges.
- Enforce clear-aisle policies to eliminate incidental forklift impacts.
- Bulk delivery
- Synchronize ロジスティクス routing with strict Warehouse management intake protocols.
- Utilize air-ride trailers to reduce transit vibration and 交通機関 shocks.
- Mandate strict “Do Not Double Stack” Can handling rules to protect bottom-layer スタッキング 誠実さ.
- FANXUN requires handling ブリキ缶 with the precision of engineered components, not bulk commodities.
- Synchronize ロジスティクス routing with strict Warehouse management intake protocols.
Bulk Order Tips For OEM Buyers
Unmanaged bulk procurement yields SKU bloat, specification drift, and dimensional mismatches at the filling line. This framework rationalizes ブリキ缶 purchasing to protect margins. FANXUN partners with OEM buyers to lock down specifications, compress SKUs, and guarantee frictionless line operations.

Negotiating Gauge (厚さ) and Volume Capacity for Cost Savings
- Negotiation relies on a unified, locked 材質仕様 document detailing exact ブリキ缶 公差.
- Gauge alignment: Match steel ゲージ そして 厚さ (例えば。, 0.19mm vs 0.22mm) precisely to burst thresholds, avoiding costly over-engineering.
- Geometry optimization: 調整する 音量 そして 容量 via specific dome profiles and neck-ins to reduce raw material weight while retaining axial strength.
- Standardization drives volume discounts.
- Consolidate around 3-4 approved ブリキ缶 フォーマット (bodies and ends) to eliminate bespoke tooling resets.
- Reject minor aesthetic trim changes that trigger tooling fees and destroy 費用対効果.
- Tactical cost controls:
- Request matrix pricing mapped to specific steel thickness tiers.
- Leverage aggregate annual volumes in negotiation, utilizing JIT (Just-In-Time) リリース.
Containerization Strategies to Optimize Shipping and Storage Requirements
Inefficient コンテナ化 のために ブリキ缶 ships dead air and invites crush damage. 最適化された パッケージデザイン maximizes freight density.
- Tactical コンテナ化 そして freight optimization:
- Calibrate can diameter-to-carton ratios to maximize 40ft container payload weight vs. cube limits.
- Specify high ECT corrugated boards; weak secondary packaging collapses under load in 倉庫保管.
- のために パレット化 そして ロジスティクス 効率:
- Enforce standard CHEP/GMA pallet footprints across all SKU variations.
- Lock layer-pad configurations to prevent dock workers from compromising load stability.
- Mandate rigid stretch-wrapping tensions and physical corner protection.
品質保証: Regulatory Compliance and Coating Adhesion Checks
Discovering defects during active filling destroys margins. のために ブリキ缶, preemptive validation is mandatory.
- 品質保証 documentation mandated for inbound receipt:
- Market-specific 規制遵守 dossiers (例えば。, FDA/EFSA food-contact).
- Validated 認定 for BPA-NI status and steel temper.
- Statistical Process Control (SPC) 縫い目 検査 logs demonstrating CPK >1.33.
- Coating controls preventing catastrophic delamination:
- Demand cross-hatch コーティングの密着性 testing integrated into factory テストプロトコル.
- Validate oven dwell times/temperatures to ensure 材料の完全性 against specific solvent 推進剤.
- Mandate accelerated aging tests utilizing actual fill chemistry.
- Safety expectations:
- Synchronize burst and leak 安全基準 between the buyer, the contract filler, and the manufacturer to prevent liability disputes.
Streamlining Supply Chain Management with Packaging Configuration Tools
Managing high-volume ブリキ缶 without digital oversight creates supply chain friction. FANXUN leverages standardized configurations to streamline procurement.
- 展開する packaging configuration software to lock primary dimensions:
- Standardize 1-inch valve cups, target heights, and flange widths—code once, deploy globally.
- Establish pre-approved secondary suppliers to ensure continuity when primary capacity tightens.
- Integrate tooling directly to サプライチェーン 実行:
- Implement automated 在庫管理 parameters to eliminate obsolete can stockpiles.
- Utilize predictive lead-time dashboards to trigger 調達 before safety stock depletes.
- Operational simplicity at the facility level:
- Management tools must generate inbound ASN (Advanced Shipping Notice) data supporting direct-to-line 物流の最適化.
- 展開する オートメーション via ERP/API links to eliminate manual data entry errors.
- 同期 digital platforms directly to dock scheduling, ensuring pallets arrive exactly when floor space is available.
金属包装のニーズに応える FANXUN との提携
漏れの心配はもうやめましょう, weak seams, and supply chain bottlenecks. FANXUNさん 30,000+ m² facility in Guangzhou integrates 100% 自動シールテスト, lab checks every 2 時間, そして ISO 9001-certified 品質管理. 必要かどうか エアゾール缶, エンジンオイル缶, または paint pails, we export seamlessly to over 80 国.
Take the next step in packaging reliability:
- ⏱️ Inquiries answered within 12 時間
- 📦 Request Free Samples 選択したアイテムについて
- 📞 Contact Us Today to secure your 1-day solution proposal.
参考文献
- そして/わかった – phmsa.dot.gov
- cold-rolled – ワールドスチール.org
- food-contact – fda.gov
- 電気めっき – pfonline.com
- BPA-IN – efsa.ヨーロッパ.eu
- リソグラフィー – piworld.com
- CTP (Computer-to-Plate) – ウィキペディア.org
- Thermal expansion – engineeringtoolbox.com
- Edge Crush Test (ECT) – packsize.com
- Statistical Process Control (SPC) – asq.org
- CPK – isixsigma.com
- ISO 9001-certified – iso.org